Start with the job decision
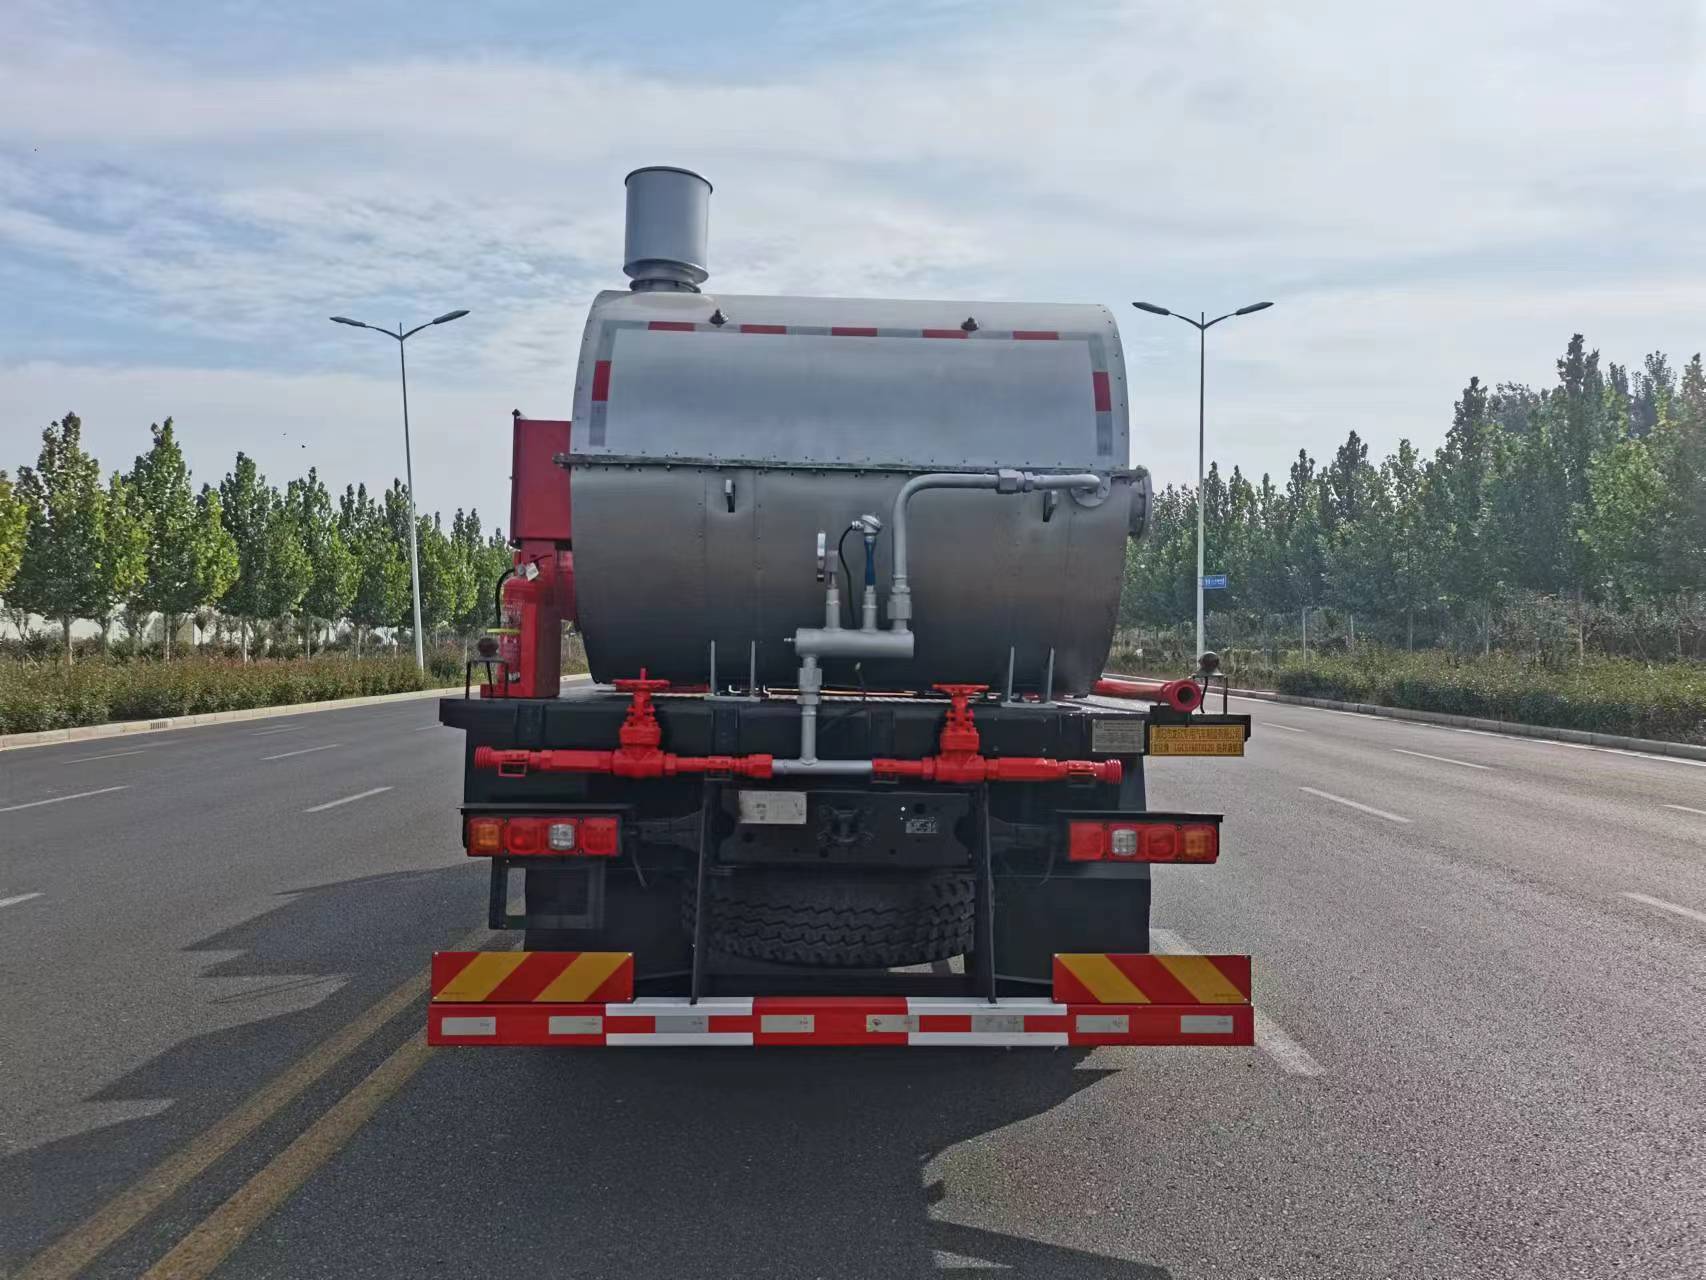
Hot Oil Flushing Unit projects succeed when the equipment scope is tied to a defined operating duty: heating and circulating oil or compatible fluid to dissolve paraffin and restore flow through wells and production lines. A useful project document separates normal duty, maximum credible duty, standby or transient conditions and the physical interfaces available at site. This keeps procurement language connected to field reality.
Record target outlet temperature, circulation pressure, required flow rate and fluid compatibility as ranges rather than isolated peak figures. The supplier can then explain how the high-efficiency coil heater, triplex circulation pump, insulated fluid tank and temperature and flame-safety controls work together across the intended envelope.
Agree the FAT plan before manufacturing is complete
The inspection and test plan should identify hold points, witness points, acceptance criteria, required instruments and records. A FAT is not simply a visual factory visit. It should verify that the manufactured package matches approved documents and that controls and protection functions behave as agreed.
| Review item | What to confirm | Evidence or input |
|---|---|---|
| high-efficiency coil heater | Model, materials, assembly and accessibility | Approved data sheet and inspection record |
| triplex circulation pump | Rotation, alignment, leakage and functional response | Test procedure and measured results |
| insulated fluid tank | Capacity, cleanliness, connections and service access | Drawing review and functional check |
| temperature and flame-safety controls | I/O, alarms, trips and event records | Cause-and-effect test sheet |
Functional tests should follow the operating sequence
Test permissives, startup logic, normal control, alarms, controlled shutdown and emergency shutdown in a sequence that operators can recognize. Simulate relevant low, high and signal-failure conditions. If full-load testing is not practical at the factory, document the limitation and define the site acceptance test that will close it.
Do not release shipment with undocumented gaps
Compile signed test sheets, material and calibration records, final drawings, manuals, spare-parts lists, packing lists and the punch list. Classify open items by whether they prevent shipment, prevent installation or may be closed during commissioning. Photographs help, but they do not replace signed acceptance records.
Keep a usable project record
Maintain one controlled file containing the approved duty sheet, supplier clarifications, drawings, component data, inspection records, test results, deviations, photographs and signed acceptance documents. Record document revisions and the person responsible for each open item. This prevents the operating team from receiving a package whose final configuration differs from the information used during procurement.
The handover set should also identify installed component models, consumables, calibration intervals, recommended spares, preservation requirements and supplier support contacts. Capture baseline operating readings when the unit is accepted. Those records give maintenance personnel a reference for condition changes and allow later modifications to be reviewed against the original design basis.
Before closing the project, confirm that operators can find the startup, normal-operation, controlled-shutdown and emergency procedures relevant to their unit. Training attendance alone is not sufficient; the responsible team should demonstrate the required checks and know which conditions require escalation rather than continued operation.
Codes, standards and project requirements
Confirm the final specification and acceptance plan against the owner’s project standards, local jurisdiction and OSHA oil and gas extraction safety guidance. The applicable project documents govern whenever they are more specific.